
Automotive and transportation tubing is rarely bought as a generic commodity. A tube that looks acceptable on a drawing can still create problems if its grade, section profile, weld condition, surface, traceability, or forming tolerance does not match the actual vehicle component. Exhaust routing, decorative trim, handrails, bus and rail interiors, equipment frames, cargo hardware, and specialist fabrication each impose a different mix of corrosion, vibration, appearance, weight, and manufacturability requirements.
For buyers sourcing stainless steel tube from China, the practical task is to translate the component function into a purchase specification that a mill and fabricator can execute. This guide explains how to do that with the verified capabilities shown on TeCarve’s Oval Pipe & Tube and Special-shaped Pipe & Tube pages. It is written for procurement teams, engineers, component manufacturers, and transport-equipment fabricators who need a clear starting point for RFQs and technical review.
Where Stainless Steel Tube Fits in Automotive and Transportation Equipment
Transportation applications are diverse. Passenger vehicles may use stainless tube in exhaust assemblies, trim, roof systems, seat or interior components, and specialist fluid or sensor lines. Commercial vehicles, buses, rail vehicles, trailers, airport equipment, and material-handling fleets add structural frames, guardrails, grab rails, luggage systems, protective housings, and custom fabricated assemblies. The same part can be exposed to road splash, salt, vibration, thermal cycling, cleaning chemicals, and repeated contact by passengers or operators.
That variety is why the component’s function should lead the specification. A bright oval trim section is selected differently from a concealed bracket tube. An exhaust-related part needs its own temperature, condensate, vibration, and joining review. A handrail or visible interior tube also needs an agreed surface appearance and a reliable way to protect that finish through bending, welding, packing, and transport.
- Exhaust and heat-adjacent fabricated parts: grade, welded-tube standard, wall thickness, forming radius, weld treatment, and the actual service temperature should be reviewed together.
- Visible trim, rail, and interior hardware: profile accuracy, surface finish, scratch protection, and batch-to-batch appearance are central requirements.
- Frames, guards, and equipment structures: section geometry, wall thickness, stiffness, joining method, and corrosion environment govern the order.
- Custom brackets and housings: a special-shaped section can reduce downstream fabrication when its profile is defined clearly and verified before production.
Stainless tube does not automatically qualify a finished automotive component. The vehicle or tier supplier remains responsible for the applicable drawings, validation plan, safety requirements, and customer approvals. TeCarve holds ISO 9001, ISO 14001, and ISO 45001 certifications; these should not be represented as IATF 16949 or as a substitute for an automotive customer’s own qualification process.
Why Oval and Special-shaped Sections Matter
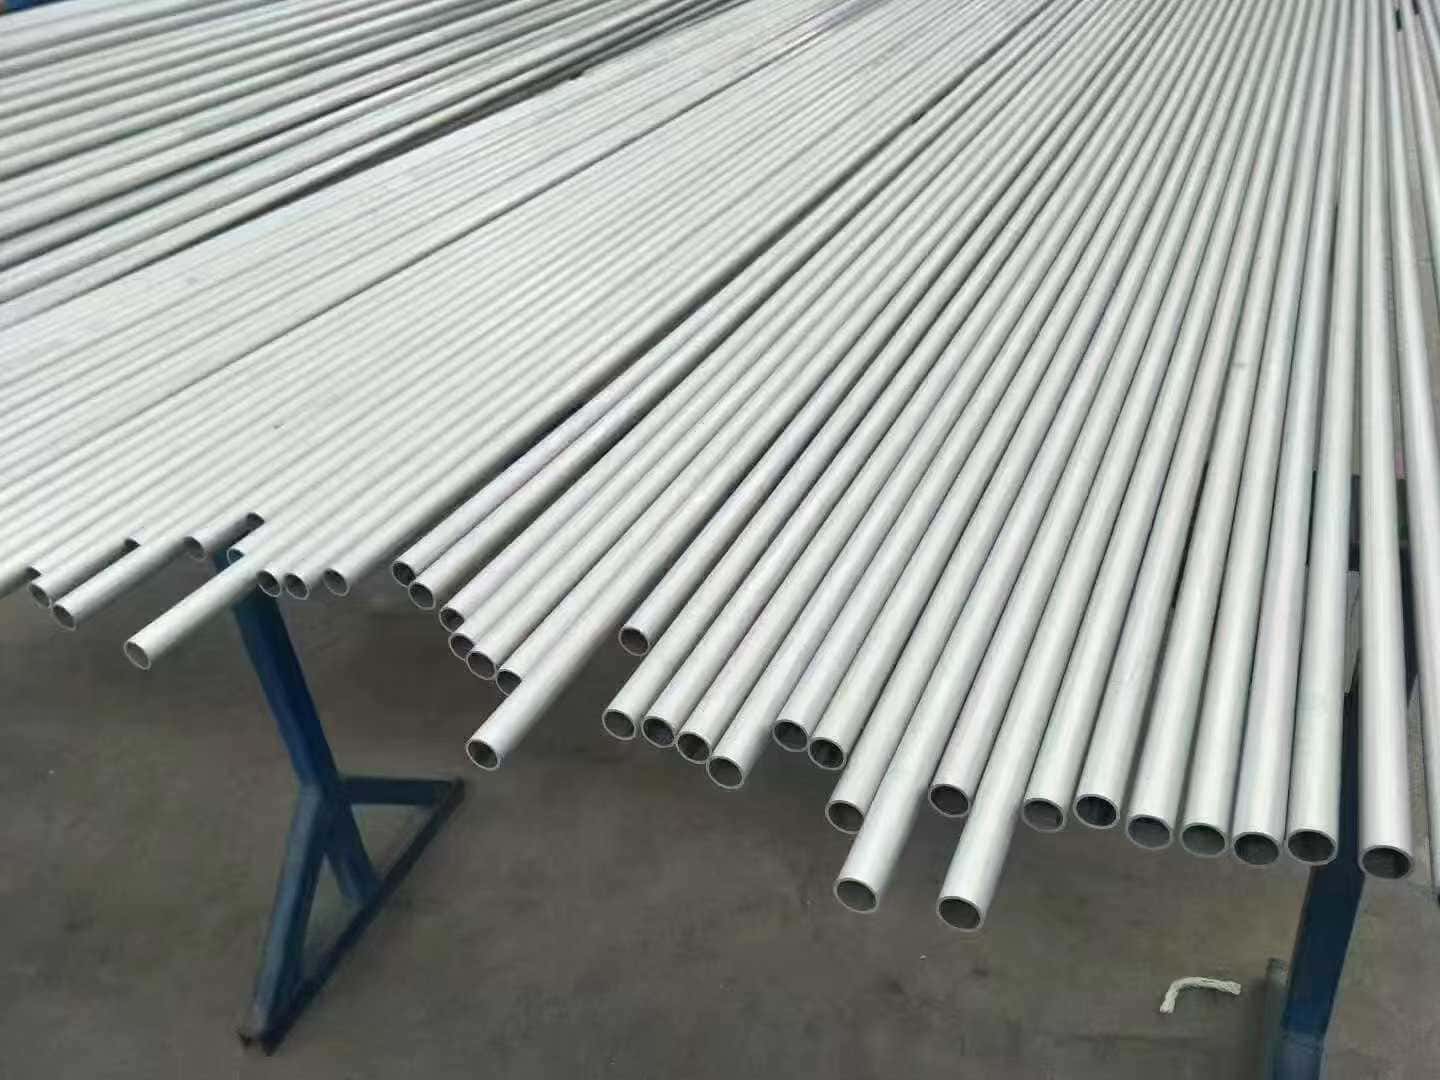
Round tube is efficient for many loads, but it is not always the most useful shape. An oval section can provide a low visual profile, directional stiffness, a smooth graspable form, and a design language suited to trims, rails, and formed assemblies. TeCarve lists oval tube dimensions from 9 × 18 mm to 100 × 150 mm, wall thickness from 0.5 mm to 3.0 mm, and lengths up to 12 metres, with customized lengths available. These values are a capability reference, not a substitute for a component drawing and tolerance schedule.
For parts with clearance restrictions or a proprietary visual shape, special-shaped tube can be specified in oval, D-shaped, triangular, and other custom profiles. TeCarve lists 0.5 mm to 5 mm wall thicknesses and 1 m to 12 m lengths for this range. Custom tooling, corner radii, straightness, twist, weld location, and cut length should be agreed before a production order. A profile drawing without those controls can leave too much interpretation at the forming stage.
Buyers should also distinguish a tube’s external envelope from its functional dimensions. A component may need a controlled internal passage, a consistent external reveal gap, a defined weld-seam orientation for bending, or a particular flat area for clips and brackets. Put those functional features directly into the RFQ. Supplying only a nominal “oval tube” description can lead to a product that is technically similar but difficult to assemble.
Grades: Match Corrosion Resistance and Formability to the Service
TeCarve’s oval range lists 201, 202, 304, 304L, 316, 316L, 409, 410, 430, and duplex grades. Its special-shaped range lists 201, 304, 304L, 316, 316L, and 430. The availability list gives a useful starting point, but grade selection must follow the exact component environment, not a marketing label.
304 and 304L
304 and 304L are common starting points where general corrosion resistance, forming, welding, and a clean finished appearance are needed. For welded fabricated assemblies, the low-carbon 304L option may be specified when the project requires it. The final choice still depends on section geometry, fabrication route, weld procedure, cleaning, and exposure. A poorly protected polished tube can be damaged in logistics regardless of its alloy grade.
316 and 316L
316 and 316L are often evaluated when chloride exposure, road salts, coastal service, or demanding cleaning conditions make a higher-corrosion-resistance option appropriate. They are not a blanket guarantee against corrosion. Deposits, crevices, standing water, temperature, surface condition, and the assembled component geometry all affect real performance. Use the material grade as one part of the engineering assessment, then confirm the actual test and acceptance criteria with the end customer.
409, 430, 201, and Other Listed Grades
Ferritic and other listed grades can be relevant to selected automotive, decorative, or cost-sensitive applications, but their use must be tied to the applicable component specification. For example, a buyer considering tube near an exhaust assembly should define the material designation, product form, test requirements, temperature exposure, and corrosion environment with the responsible design authority. Do not assume that one stainless grade is interchangeable with another because both are described as stainless steel.
Standards: Use the Right Document for the Tube’s Function
For welded mechanical tubing, ASTM A554 is particularly relevant to transportation fabrication. ASTM describes A554 as covering welded stainless steel mechanical tubing for applications where appearance, mechanical properties, or corrosion resistance are needed; its scope includes structural, exhaust, and other applications, and permits round, square, rectangular, and special shapes. That makes it a useful reference when the ordered product is a formed or fabricated mechanical section rather than pressure tubing.
TeCarve’s oval tube page lists ASTM A554, EN 10296-2, JIS G3446, GB/T 12770, and ISO 1127. The special-shaped page lists ASTM A554 / A312, EN 10296 / EN 10088, JIS G3446 / JIS G3468, GB/T 12770 / GB/T 18705, and ISO 15510. These are page-listed reference standards; the purchase order should state the exact standard and revision required for the component rather than listing a broad group of documents.
ASTM A269/A269M is a different reference used for seamless and welded austenitic stainless tubing for general corrosion-resisting and temperature service. It should be considered only where its scope and the project requirements fit the ordered tube. A standard number is not an interchangeable quality badge. The ordered standard, grade, dimensions, condition, inspection method, and documentation requirements need to agree with one another.
Surface Finish and Appearance Control
Surface is a functional requirement in transportation equipment. It affects visible quality, cleanability, corrosion initiation around scratches, coating or adhesive preparation, and the customer’s first impression. TeCarve lists annealed, pickled, polished, mirror, and satin finishes for oval tube. For special-shaped tube it lists mirror, satin, hairline, and electro-polished finishes. Specify the finish by the component’s intended function and, where appearance is important, approve a retained sample or an agreed visual standard before the production run.
An RFQ for visible tube should define more than “polished.” Include the required finish, viewing condition, permitted handling marks, protective film or wrapping, cut-end treatment, packing orientation, and whether bends or welded assemblies will be supplied. If a component will be formed after delivery, define which surface is critical and whether the weld seam needs a controlled position. This avoids a common failure mode: a tube meets basic dimensions but loses acceptance because the surface was not specified as a measurable purchase requirement.
Inspection, Traceability, and a Practical RFQ
The product pages describe dimensional consistency checks, weld-integrity testing, surface-roughness inspection, raw-material traceability, visual inspection, and surface-finish grading. Convert those capabilities into a component-specific inspection plan. Ask for the documents and hold points that matter to the job rather than assuming a generic certificate covers every risk.
- State the end application and environment, including salt, moisture, cleaning chemicals, temperature, and vibration where relevant.
- Attach a dimensional drawing with outside profile, wall thickness, length, tolerance, straightness, twist, corner radius, and weld-seam position if applicable.
- Specify grade, exact product standard, delivery condition, surface finish, and any required test method.
- Define material-traceability and inspection-document requirements before the quotation is finalized.
- For a new profile, arrange a sample, first-article review, or other agreed approval step before releasing series production.
- Describe packing requirements so finished surfaces and cut ends remain protected through export transport.
How to Review a Sample Before Series Supply
For a new transportation component, the first sample is where the written specification becomes measurable. Review it against the controlled drawing rather than against a general impression. Check the profile at the locations that matter to assembly, measure wall thickness at the relevant points, confirm cut length and straightness, and examine any area that will be bent, welded, polished, clipped, or visible after installation. If a seam is present, confirm its required position before the tube enters a downstream forming process.
Surface review deserves the same discipline. Agree on the lighting, viewing distance, protected faces, and acceptable handling marks for visible material. Mirror, satin, hairline, and electro-polished finishes can look very different after bending or fabrication, so an approved straight-tube sample may not be enough when TeCarve is supplying a further-processed part. Define whether approval applies to the incoming tube, the formed component, or both. Record the packing method as well: separator material, protective film, end caps, bundle orientation, and container handling all influence the finish received at destination.
Documentation should track the same logic. A material test certificate can support traceability, but it does not establish compliance with an unstated dimensional tolerance or an unagreed appearance criterion. The purchase order should identify the required material documentation, test reports, sample approval record, and any third-party inspection or release point. If the vehicle program requires additional customer-specific validation, plan it with the responsible tier or OEM before the commercial order is released.
These controls are especially useful when the tube is a custom profile. Custom sections can eliminate machining, weld-on tabs, or multiple assembled pieces, but they transfer more importance to the original drawing and approval cycle. Define the critical-to-function features, make a sample before committing to production volume, and retain the approved reference. This provides a repeatable route from design intent to incoming inspection and helps both buyer and supplier resolve variation using agreed evidence rather than interpretation.
From Tube Specification to Repeatable Supply
A strong transportation-tube specification does not overpromise. It identifies the real component environment, selects a grade and standard that fit that use, records the profile and tolerance requirements, and sets a clear inspection and packing plan. That approach makes technical conversations faster and reduces costly interpretation after production has started.
TeCarve can discuss oval and special-shaped stainless steel tube requirements from a component drawing or RFQ. Start with the use case, grade direction, standard, dimensions, wall thickness, surface, order quantity, and required documents. For broader application context, see TeCarve’s Automotive & Transportation industry page.