Why choose stainless steel clad pipe instead of solid stainless pipe?
The same corrosion-resistant wetted surface as a solid alloy pipe, with far less alloy per metre and a carbon steel backing that carries the pressure.
On a 1020 × 8 mm pipe, a solid 2205 pipe uses about 198 kg of 2205 per metre; a clad pipe with a 1.5 mm 2205 layer uses about 37 kg, with the rest carbon steel. The more expensive the grade (2205, 2507, 904L), the larger the difference. Send us your size and grade and we'll quote clad and solid side by side.
The process medium only touches the clad layer, so the wetted surface performs like solid pipe of the same grade. Clad thickness is sized from the medium's corrosion rate plus a corrosion allowance.
Compared with solid 304/316L pipe (minimum yield strength 205 / 170 MPa, ASTM A240), the pressure-bearing backing is Q355B (355 MPa minimum, GB/T 1591) or line-pipe steel such as L360 / X52 (360 MPa).
Handled, supported and lifted like carbon steel pipe; girth welds follow a WPS we supply with the order; OD up to 2800 mm (LSAW) / 3600 mm (rolled), lengths up to 15 m; 30–45 days lead time; trial orders of 2–5 joints.
| Metric / Property | Solid 2205 pipe | 2205-clad pipe (1.5 mm 2205 + 6.5 mm carbon steel) |
|---|---|---|
| 2205 per metre | ≈ 198 kg | ≈ 37 kg |
| Total weight per metre | ≈ 198 kg | ≈ 199 kg |
| Wetted surface | 2205 | 2205 |
| Pressure-bearing wall | 2205 | carbon steel backing |
Weights calculated from nominal dimensions (densities 7.8 / 7.85 g/cm³). Actual quotes depend on grade, size and quantity.
When Solid Pipe Is the Better Choice
- OD below 219 mm or thin walls: Small-diameter tubing and light schedules where roll-forming clad plate is impractical.
- Dual-sided corrosive exposure: Services where both inside and outside surfaces are exposed to corrosive media (the clad layer protects one side only).
- Solid-alloy specifications: Critical services and client codes that explicitly call for a solid-alloy specification throughout.
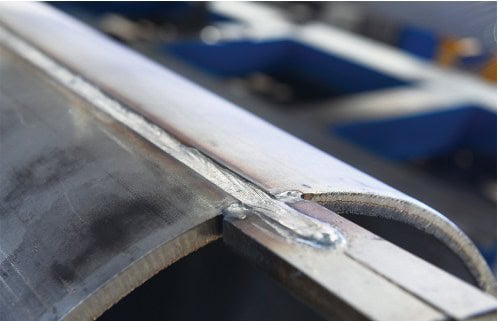
Cost-Effective Bimetallic Stainless Steel Clad Pipes for Severe Environments
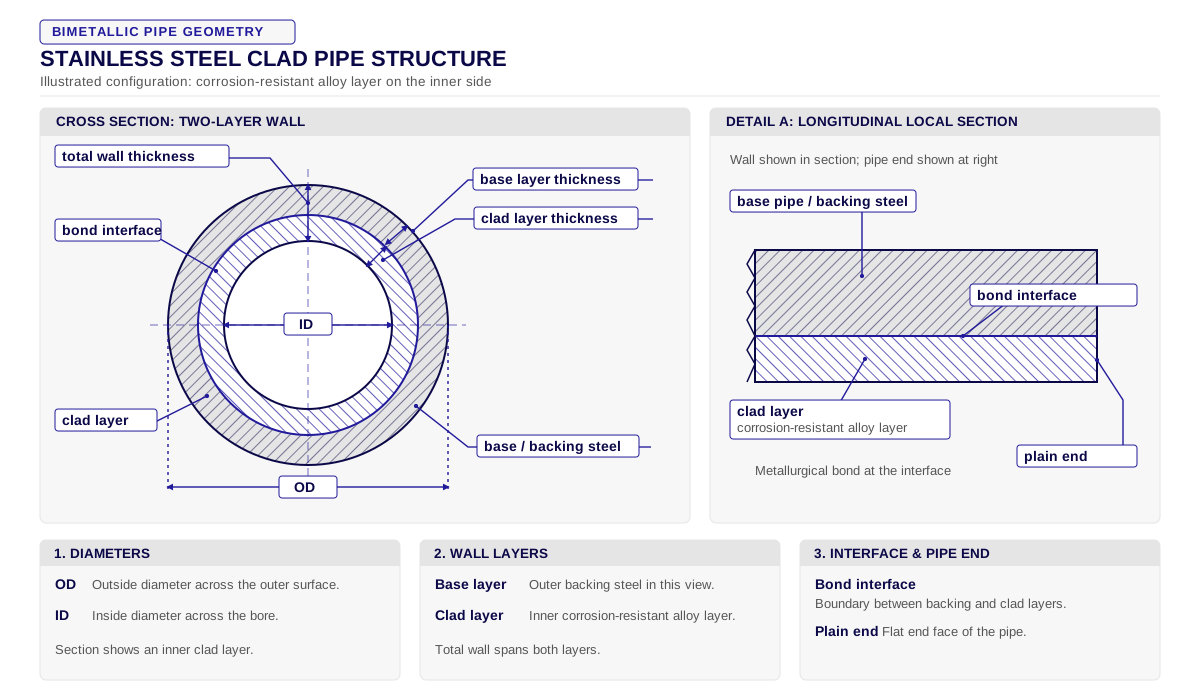
Clad Pipe Structure Explained
1. Engineering Comparison: Metallurgical Clad Pipe vs Lined Pipe vs Solid Alloy Pipe
When specifying corrosion-resistant piping for severe process duties, engineers compare whether a stainless steel clad pipe, a mechanically lined pipe, or a solid alloy pipe best meets project mechanical, hydraulic, and commercial requirements. A mechanically lined pipe relies on an interference fit between liner and host pipe; a bimetallic clad pipe has a metallurgical bond between the two layers.
| Feature / Parameter | Metallurgical Clad Pipe (TeCarve) | Mechanically Lined Pipe | Solid Alloy Pipe |
|---|---|---|---|
| Bond type | Metallurgical bond at the interface; bond shear strength tested per ASTM A264. | Mechanical interference fit; no metallurgical bond between CRA liner and outer carbon steel host pipe. | Homogeneous single alloy throughout the entire wall thickness; no interface. |
| How it is made | Formed from hot-roll-bonded (or explosion-bonded) clad plate, followed by longitudinal (LSAW), spiral (SSAW), or heavy-wall rolled seam welding. | CRA liner expanded into a carbon steel host pipe using mechanical expansion or hydraulic sizing. | Hot extruded or cold drawn seamless pipe, or roll-formed and seam-welded from solid alloy plate. |
| Behaviour under bending & installation | Behaves as one integral wall; there is no separate liner that could wrinkle or collapse during bending. | The liner can wrinkle, buckle, or collapse inward under plastic bending, offshore reeling, thermal cycling, or severe internal vacuum. | Uniform bending and deformation response governed entirely by the selected alloy's mechanical properties. |
| Weld joint | Standard full-penetration butt weld: carbon steel backing pass, alloy transition buffer pass, and matching alloy cap on clad side per qualified WPS; no internal liner sleeve. | Requires internal seal-weld overlay, weld overlay of pipe ends, or specialized CRA sleeve fittings to protect the unbonded seam. | Standard full-penetration butt weld using matching alloy filler metal throughout the entire joint. |
| Typical use | Chemical and coal-chemical process piping, blast-furnace gas lines, seawater desalination, municipal water and district heating networks, shipbuilding seawater piping, pressure vessels. | Pipelines and flowlines where the liner design, installation method and operating conditions have been qualified for a mechanical bond. | Small and medium diameters, and services where a carbon steel backing is not acceptable. |
| Relative alloy content | Optimized material utilization: only the corrosion-resistant layer — typically 1.5–3 mm — is stainless or duplex, while the structural backing is carbon steel (roughly 80% of the pipe's weight is carbon steel on a 1020 × 8 mm pipe with a 1.5 mm 2205 layer). | Low alloy fraction (thin CRA liner inside a carbon steel host pipe). | 100% solid corrosion-resistant alloy throughout the entire wall thickness. |
2. Girth Weld Sequence: Field Joining Procedure for CRA Clad Pipe
Proper field girth welding of clad steel pipe requires a qualified 3-step welding sequence to maintain structural containment on the backing side and continuous corrosion resistance across the weld seam. Dilution between base carbon steel and the CRA cladding must be strictly controlled.
Carbon-Steel Root & Fill Passes
Weld the base carbon steel from the backing side using matching carbon steel consumables. The root and fill passes provide the primary mechanical and pressure-containment strength.
Buffer (Transition) Layer
Apply an over-alloyed buffer pass across the clad/base interface. The over-alloyed buffer compensates for dilution from the carbon steel so the deposit does not form brittle martensite.
Matching Alloy Cap Pass
Deposit the final capping pass on the clad side using matching alloy consumables, ensuring an unbroken, flush corrosion barrier matching the parent cladding alloy.
| Clad Alloy Grade | Buffer (Transition) Layer Consumable | Clad-Side Capping Layer Consumable | Consumable Note |
|---|---|---|---|
| 304L Clad | ER309L | ER308L | Typical; final consumables per the qualified WPS/PQR |
| 316L Clad | ER309MoL | ER316L | Typical; final consumables per the qualified WPS/PQR |
| 2205 Clad | ER2209 | ER2209 | Typical; final consumables per the qualified WPS/PQR |
| Other Grades | per WPS | per WPS | Consumables determined per qualified project WPS/PQR |
* Note: Welding consumables listed are typical recommendations. Final filler metals, preheat temperatures, and interpass controls must strictly follow the qualified Welding Procedure Specification (WPS) and Procedure Qualification Record (PQR) approved for the project.
3. Dimensional Reference: Nominal Pipe Size (NPS) to Metric Outside Diameter (OD)
TeCarve supplies stainless steel clad pipe across standard ASME B36.10 nominal sizes and custom heavy-wall dimensions. Available pipe manufacturing processes depend on outer diameter, wall thickness, and project quantities:
| NPS (inch) | OD (mm) | Available Forming Processes | Process Capability Coverage |
|---|---|---|---|
| NPS 8 | 219.1 | SSAW | SSAW (OD 219–1620 mm) |
| NPS 10 | 273.1 | SSAW | SSAW (OD 219–1620 mm) |
| NPS 12 | 323.9 (Chinese standard OD 325) | SSAW, LSAW | SSAW (OD 219–1620 mm), LSAW (OD 325–2800 mm) |
| NPS 14 | 355.6 | SSAW, LSAW | SSAW (OD 219–1620 mm), LSAW (OD 325–2800 mm) |
| NPS 16 | 406.4 | SSAW, LSAW | SSAW (OD 219–1620 mm), LSAW (OD 325–2800 mm) |
| NPS 18 | 457 | SSAW, LSAW | SSAW (OD 219–1620 mm), LSAW (OD 325–2800 mm) |
| NPS 20 | 508 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 24 | 610 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 28 | 711 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 32 | 813 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 36 | 914 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 40 | 1016 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 48 | 1219 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 56 | 1422 | SSAW, LSAW, Rolled | SSAW, LSAW, Rolled (OD 500–3600 mm) |
| NPS 64 | 1626 | LSAW, Rolled | LSAW (OD 325–2800 mm), Rolled (OD 500–3600 mm) |
| NPS 72 | 1829 | LSAW, Rolled | LSAW (OD 325–2800 mm), Rolled (OD 500–3600 mm) |
| NPS 80 | 2032 | LSAW, Rolled | LSAW (OD 325–2800 mm), Rolled (OD 500–3600 mm) |
Process capability summary: SSAW available for OD 219–1620 mm; LSAW available for OD 325–2800 mm; heavy-wall rolled available for OD 500–3600 mm. Larger diameters up to 2800 mm (LSAW) and 3600 mm (rolled) made to order (total wall thickness up to 100 mm for rolled pipe).
TeCarve's clad pipe is supplied as roll-formed, welded pipe made from clad plate to ASTM A264 / GB/T 8165. It is not supplied to API 5LD; if your project specifies API 5LD, tell us at inquiry so we can confirm before quoting.
Get Your Stainless Steel Clad Pipe Quote
Sourcing metallurgically bonded stainless steel or duplex clad pipe for chemical process lines, blast-furnace gas, seawater desalination, or heavy-wall structural projects? Contact our sales engineering desk for pricing, clad layer and base metal optimization, welding procedure support, and flexible project trials (1 ton or 100 m MOQ, 2–5 joints prototype).
Engineering review of your size, grade and medium, with clad and solid alloy quoted side by side.
Clad ring sections and cut pipe samples provided for metallurgical bond inspection, welding trials, and laboratory testing.
Verify field weldability, dimensional fit, and corrosion performance with flexible 1 ton or 100 m trial orders (2–5 joints).
Ultrasonic bond inspection of the clad plate, weld-seam RT/UT and hydrostatic testing to your specification, EN 10204 3.1 certificates for clad and base layers.
Stainless Steel Clad Pipe Product & Application Photos
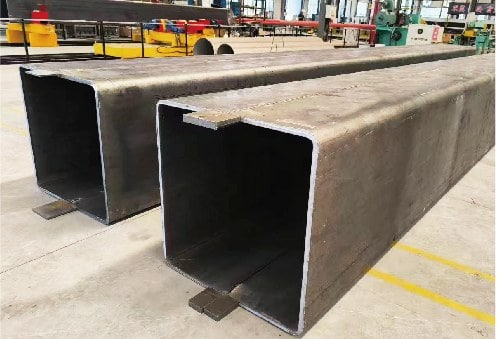
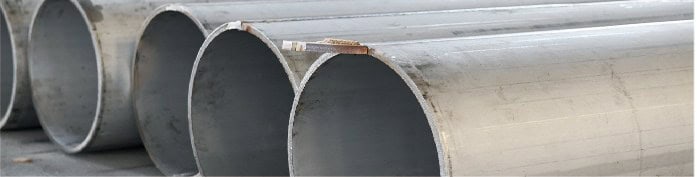
The photos show square tube products, inspection, packaging and loading.
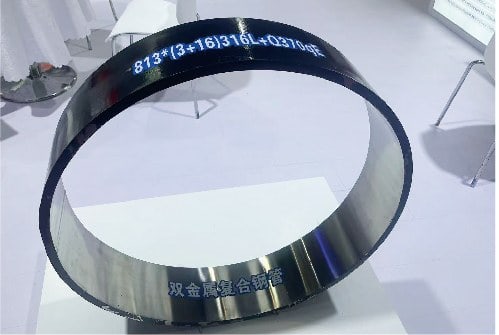
How your order is made, checked and shipped
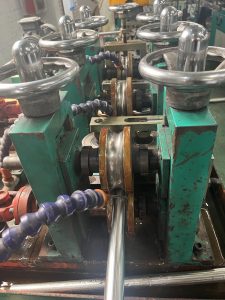
Tube forming at the dedicated plant
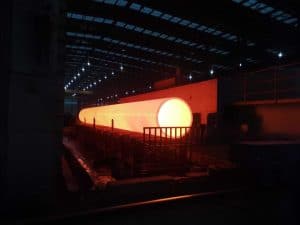
Heat treatment (annealing)
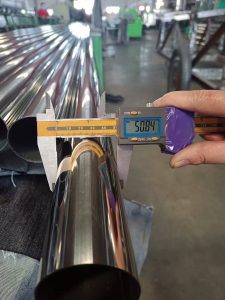
Dimensional inspection
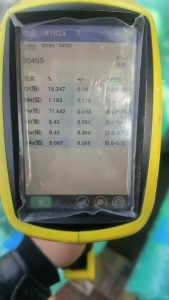
Alloy verification with a handheld analyzer
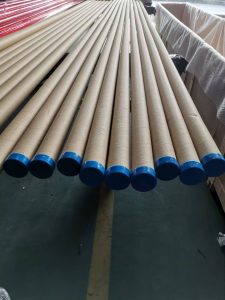
Export packing
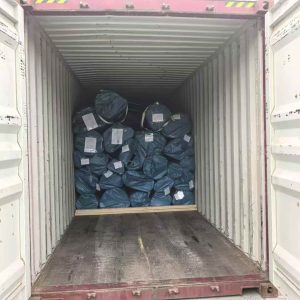
Container loading
What Overseas Buyers Say About TeCarve Tubing
“I've received the goods and everything is fine.”
“The goods already send to customers. I am waiting for the next order from them.”
“…there is no need of inspection this time… I trust in your product.”
Frequently Asked Questions
Stainless steel corrugated pipe is used in flexible connections and exhaust flex joints.
Oval stainless steel tube has an elliptical cross-section.
Stainless steel capillary tube is used in medical devices and analytical instruments.
A helical coil tube is a stainless steel tube wound into a helical coil.
Special-shaped tubing includes oval and D-shaped profiles.
Sanitary stainless steel tube is used in food and beverage processing.
Stainless steel square tubes are used in structural and architectural applications.
What is a stainless steel clad pipe and how is it constructed?
A stainless steel clad pipe is a bimetallic composite pipe consisting of an inner or outer corrosion-resistant stainless steel or duplex alloy layer metallurgically bonded to a high-strength carbon or low-alloy steel backing. Produced by the Foshan plant from metallurgically bonded clad plate, it provides the corrosion resistance of solid alloy on the wetted process face while utilizing economical carbon steel for structural pressure containment. Available in two-layer and three-layer configurations, forming types include longitudinal submerged arc welded (LSAW), spiral submerged arc welded (SSAW), heavy-wall rolled pipe, and structural square or rectangular tubing.
What alloy grades and base materials are available for clad pipes?
Clad layers are supplied in austenitic and duplex grades including 304, 304L, 316L, 321, 310S, 317L, duplex 2205, super duplex 2507, and 904L. Base metal carbon and alloy steels include structural grades Q235B, Q355B, Q390B–Q690B, boiler and pressure vessel grades Q245R–Q370R, SA516 Gr.70, and line pipe grades L245–L555 (X52–X70). Thin-wall composite tubing pairing 201, 304, or 316 with Q235 or Q355 is also available for guardrails, bridge railings, and industrial conveyor rollers.
How does the corrosion resistance and service life of clad pipe compare to solid stainless steel pipe?
The process medium only ever touches the clad layer, so corrosion resistance on the wetted surface matches a solid pipe of the same grade. Service life is engineered, not guessed: we size the clad thickness from your medium's corrosion rate plus a corrosion allowance. Tell us the medium — chlorides, H₂S, pH, temperature — and we'll recommend a grade and layer thickness. In a one-year side-by-side trial on a steelworks blast-furnace gas line, the carbon steel section showed heavy corrosion and leaks, while the clad pipe section showed no pitting or delamination.
What is the cost and weight advantage of clad pipe compared to solid alloy pipe?
Only the corrosion-resistant layer — typically 1.5–3 mm — is stainless or duplex. The rest of the wall is carbon steel. On a 1020 × 8 mm pipe with a 1.5 mm 2205 layer, roughly 80% of the pipe's weight is carbon steel. The higher the alloy grade (2205, 2507, 904L), the bigger the gap versus a solid pipe. Send us your size and grade and we'll quote clad and solid side by side.
What size ranges and dimensions does TeCarve supply for stainless steel clad pipe?
The Foshan plant fabricates clad pipe across a broad dimensional matrix: longitudinal submerged arc welded (LSAW) bimetallic clad pipe in outer diameter (OD) 325 mm to 2800 mm with total wall thickness 5 mm to 70 mm; spiral welded (SSAW) clad pipe in OD 219 mm to 1620 mm with wall thickness 5 mm to 25 mm; heavy-wall rolled clad pipe in OD 500 mm to 3600 mm with wall thickness 8 mm to 100 mm; and clad square/rectangular tubing from 200 × 200 mm to 3000 × 3000 mm with wall thickness 6 mm to 40 mm. Clad layer thickness is typically 1.5 mm to 3 mm. Standard delivery lengths range from 6000 mm to 15000 mm.
What manufacturing standards and testing specifications apply to clad pipe?
Clad pipes are manufactured from clad plate to ASTM A264 / GB/T 8165 and pressure vessel clad plate standard NB/T 47002, with GB/T 12771 referenced for welded tube requirements. Quality control includes ultrasonic inspection of the clad-plate bond (ASTM A578 / NB/T 47002), shear strength testing of the bond per ASTM A264, and hydrostatic testing and RT/UT of weld seams to the scope set by the project specification, and mill test certificates (EN 10204 3.1) for both base and clad layers.
How are girth welds and pipe ends joined during field installation?
Girth welds need a stainless/alloy filler pass over the clad side so the corrosion barrier stays continuous; pipe ends are seal-welded. We supply a recommended welding procedure (WPS) with the order. Welded pipe joints can be configured with plain ends, beveled ends with seal welding, or customized flanged connections to integrate seamlessly with existing process piping and equipment nozzles.
What are the primary industrial applications for stainless steel clad pipes?
Stainless steel clad pipe is primarily used in chemical and coal chemical process piping, blast-furnace gas lines and flue gas ducting, seawater desalination and marine intake piping, municipal water transmission and district thermal heating networks, pressure vessel shells and nozzles, and architectural infrastructure such as bridge railings, riverside safety guardrails, and heavy conveyor rollers.
What is the difference between clad pipe and lined pipe?
The difference is the bond. In clad pipe the corrosion-resistant alloy layer is metallurgically bonded to the carbon steel backing (by hot-roll or explosion bonding of the plate). In contrast, a mechanically lined pipe relies on a mechanical interference fit with no metallic bond between the liner and outer pipe. Under plastic bending, offshore reeling, thermal cycling, or internal vacuum conditions, a mechanical liner risks wrinkling, buckling, or collapsing inward. Clad pipe is chosen where bending, thermal cycling or vacuum make a separate liner a risk.
Is TeCarve stainless steel clad pipe supplied to API 5LD?
No. TeCarve's clad pipe is roll-formed and seam-welded from clad plate made to ASTM A264 / GB/T 8165; it is not supplied to API 5LD. If your project specifies API 5LD, tell us at inquiry so we can confirm before quoting.
What are the cost advantages of stainless steel clad pipe?
Clad pipe uses structural carbon steel for external pressure containment and a stainless alloy liner for corrosion resistance. This provides the corrosion performance of solid stainless pipe at reduced material cost for large-diameter lines.
How is interlayer bonding and seam integrity verified for clad pipe?
Clad plates undergo ultrasonic bond inspection conforming to ASTM A578 and NB/T 47002, followed by radiographic (RT) or ultrasonic (UT) inspection of longitudinal weld seams.