
Pressure-Tight Heat Exchanger Tubes: 100% Hydrostatic & 100% Eddy-Current Tested
ASTM A213 seamless and ASTM A249 welded heat exchanger straight tubes and precision U-bends from our Foshan and Wenzhou partner factories.


Get Your Heat Exchanger Tube Quote
Sourcing precision stainless steel heat exchanger tubing (straight or U-bent) for shell-and-tube heat exchangers, surface condensers, boilers, or chemical chillers? Contact our thermal engineering desk for live mill pricing, tight wall tolerances, custom cut lengths, and flexible trial orders (100–300 kg MOQ supported).
Immediate heat exchanger tube pricing, production schedule planning, and raw billet stock checks within 2 hours.
Short tube cuts provided for tubesheet roller expansion testing, orbital seal weld trials, and metallography.
Verify tubesheet hole fit, baffle clearance, or bundle assembly parameters with low-MOQ trial orders.
100% Eddy-Current / Hydrostatic testing, flattening, flaring, reverse-bend tests, and full 3.1 certification.
For critical heat exchanger and condenser bundles, explore how engineers and procurement teams can verify our partner factories’ testing, hydro-test parameters, eddy current inspection, and MTC documentation prior to shipment.
What Quality Tests Does TeCarve Heat Exchanger Tube Pass Before Delivery?
Every heat exchanger tube batch runs 100% flattening, flaring/expansion, and bending tests to confirm the tube can go through tube-to-tubesheet expansion (tube expanding) in the field without cracking; welded heat exchanger tube additionally gets a reverse flattening test on the weld seam. This is on top of the 100% eddy current and hydraulic proof testing already covered above.
For projects specifying it, an intergranular corrosion (IGC) test to ASTM A262 (Practice E or Practice A) or GB/T 4334 can also be performed — this is a project-specified test rather than a standard default on every order, so flag it at inquiry stage if your specification requires it.
Why Would a Heat Exchanger Tube Fail a Hydrostatic Pressure Test?
A hydrostatic test rarely creates a problem — it reveals one that already existed. Common root causes include pitting or crevice corrosion that has locally thinned the wall, stress corrosion cracking from chloride exposure (cracks can be invisible before pressure is applied), weld or fabrication defects, wrong alloy for the service environment, and mechanical wear at baffles or tube-to-tubesheet joints from vibration.
Because these defects are often not visible before testing, TeCarve runs 100% eddy current and hydraulic proof testing on every heat exchanger tube batch, plus PMI (positive material identification) and chemical composition analysis to confirm the correct alloy was actually supplied — catching wall-thinning and material-grade mismatches before they reach a customer's pressure test.
Heat Exchanger Tube Factory & Inspection Photos
Real product, inspection, packaging and loading photos.
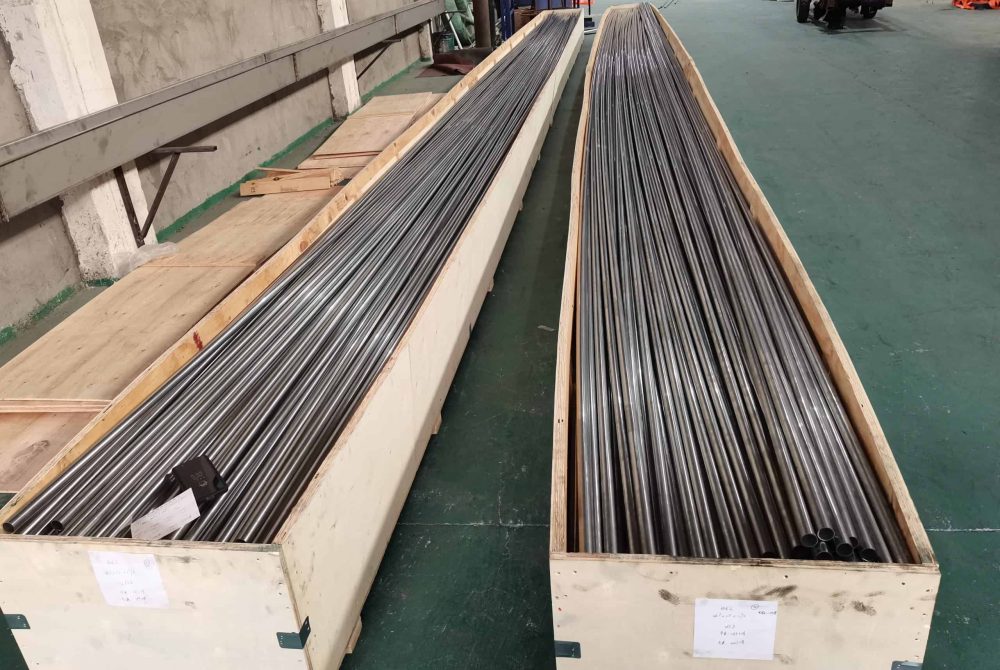
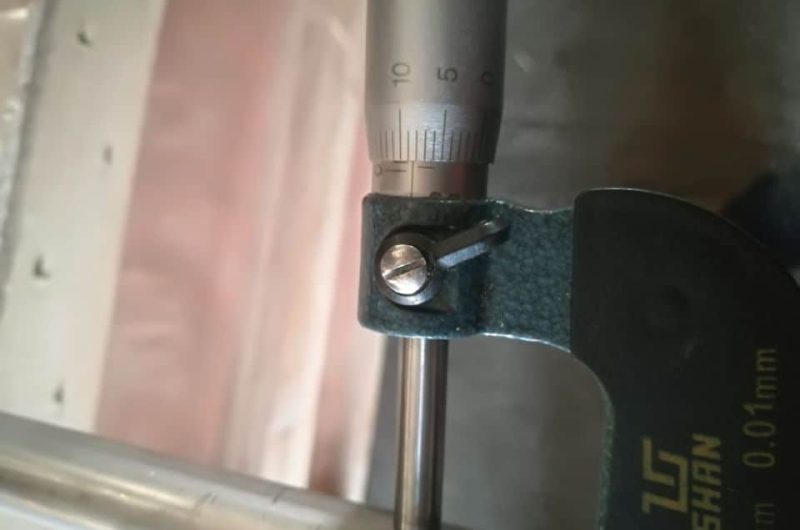
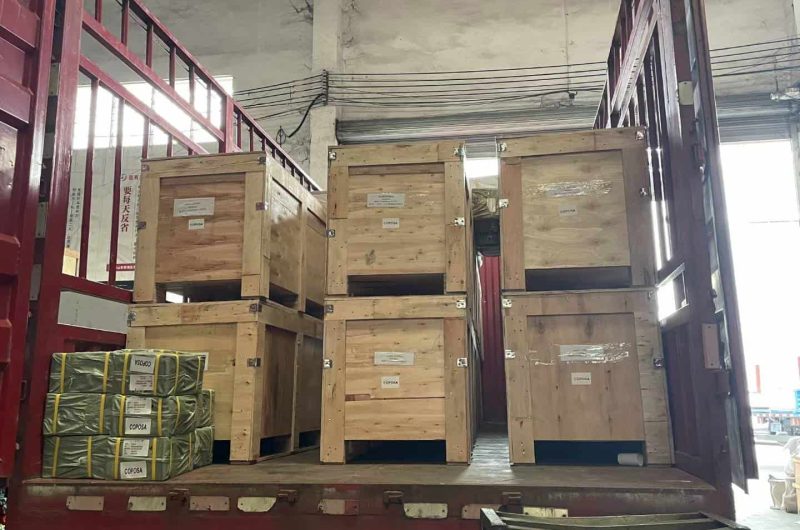
How your order is made, checked and shipped

Tube forming at the partner factory

Heat treatment (annealing)

Dimensional inspection

Alloy verification with a handheld analyzer

Export packing

Container loading
What Global Buyers Say About TeCarve Tubing
“I've received the goods and everything is fine.”
“The goods already send to customers. I am waiting for the next order from them.”
“…there is no need of inspection this time… I trust in your product.”
Frequently Asked Questions
What standards apply to stainless steel heat exchanger tubes?
Our heat exchanger tubes comply with ASTM A213 (seamless), ASTM A249 (welded), TEMA standards for shell-and-tube exchangers, EN 10216-5, and EN 10217-7. Available in grades TP304, TP304L, TP316, TP316L, TP321, TP347, and duplex 2205/2507.
What is the size range for heat exchanger tubes?
Standard heat exchanger tube ODs range from 6 mm to 101.6 mm with wall thickness 0.5 mm to 4 mm. U-bend tubes and custom straight lengths are manufactured to TEMA or customer exchanger drawings.
What types of heat exchanger tubes does TeCarve supply?
We supply straight tubes, U-bend tubes, and low-fin tubes for shell-and-tube heat exchangers, condensers, reboilers, and coolers. All tubes undergo hydraulic proof testing; eddy-current NDT is available on request.
How do I choose between seamless and welded heat exchanger tubes?
Seamless tubes are preferred for high-pressure, high-temperature, or corrosive service where seam integrity is critical. Welded-and-drawn (W&D) tubes meet the same ASTM A249 standards and are a cost-effective alternative for the majority of heat exchanger applications.
What testing and documentation is provided with heat exchanger tubes?
Each batch is supplied with a full Mill Test Certificate (EN 10204 3.1) covering chemical analysis, mechanical properties, and heat number traceability. Proof pressure, flaring, flattening, and eddy-current NDT reports are available per ASTM and TEMA requirements.
Does TeCarve perform both hydrostatic and eddy current testing on heat exchanger tubes?
Yes. While ASTM A249 Section 13.6 and JIS G3463 permit choosing either hydrostatic or nondestructive electric testing, every TeCarve heat exchanger tube receives both 100% hydrostatic testing and 100% eddy current testing before dispatch.
What mechanical and corrosion tests are conducted on heat exchanger tubes?
We perform 100% flattening, flaring (expansion), and bending tests, plus reverse flattening on welded tubes. Intergranular corrosion testing per ASTM A262 Practice E or A is available on request.
Can TeCarve supply U-tubes bent to customer drawings?
Yes. We supply U-bent heat exchanger tubes formed to customer bending schedules, drawings, and radius tables.