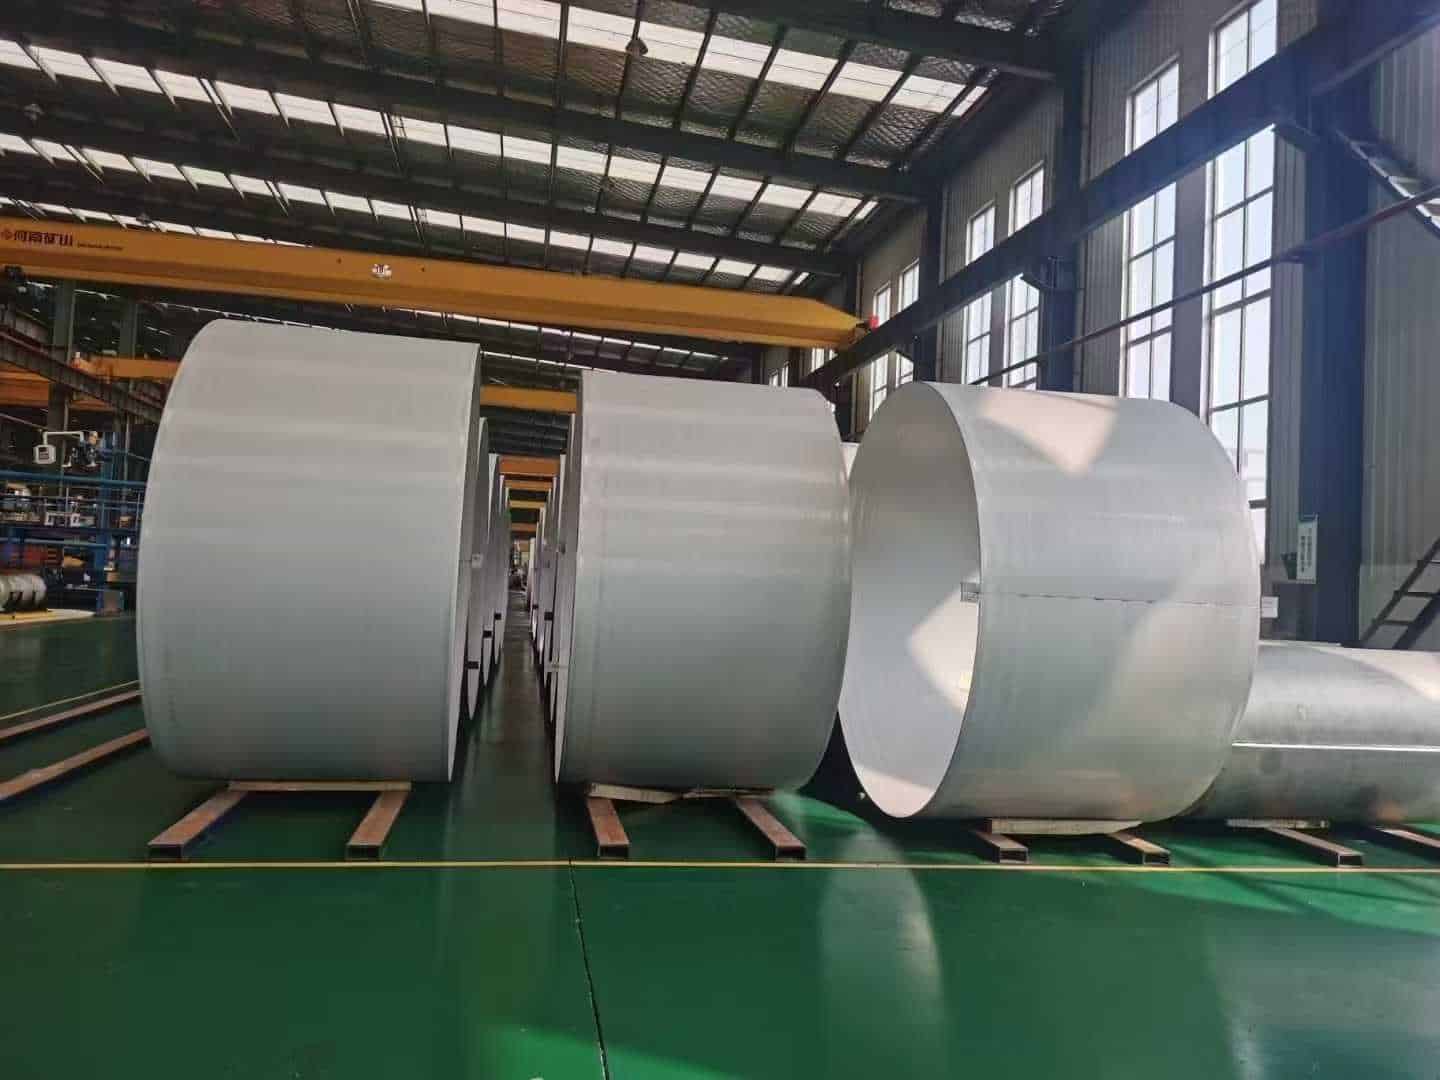

ASTM A358/A358M is the standard specification for electric-fusion-welded (EFW) austenitic chromium-nickel stainless steel pipe for high-temperature and corrosive service. Formed from ASTM A240/A240M plate with filler metal added, it defines five pipe classes based on joint design and radiography. Summary based on ASTM A358/A358M-15; later editions may differ — refer to the purchased standard for the full text.
Key Takeaway: What Does ASTM A358 Cover?
ASTM A358 covers electric-fusion-welded austenitic chromium-nickel stainless steel pipe made from A240 plate, for corrosive or high-temperature service, or general applications. The five classes govern joint type and radiography: Class 1 (double-welded, complete RT), Class 2 (double-welded, no RT), Class 3 (single-welded, complete RT), Class 4 (single-welded, inside pass may be made without filler, complete RT), and Class 5 (double-welded, spot RT ≥12 in [300 mm] per 50 ft [15 m]). Grade and heat treatment are chosen by purchaser.
1. Scope and Applicable Standards
Under Clause 1.1, ASTM A358 covers electric-fusion-welded austenitic chromium-nickel stainless pipe for corrosive, high-temperature, or general service. Unlike pipe continuously formed from strip without filler metal, A358 pipe is fabricated from plate with straight longitudinal butt joints welded per ASME BPVC Section IX.
Clause 1.2 leaves grade and heat treatment to purchaser discretion. Clause 1.4 provides eight supplementary requirements (S1–S8). Clause 1.5 designates inch-pound units as standard unless metric “M” is specified. General delivery requirements follow ASTM A999/A999M (Section 5). The ASME counterpart is ASME SA-358 (ASTM Committee A01/Subcommittee A01.10).
2. The Five ASTM A358 Pipe Classes
Under Clause 1.3, ASTM A358 categorizes pipe into five classes based on welding configuration, filler metal addition, and radiographic examination:
| Class | Welding Joint Type | Filler Metal Deposition | Radiographic Examination |
|---|---|---|---|
| Class 1 | Double-welded butt joint | Filler metal in all passes | Completely radiographed per ASME VIII UW-51 |
| Class 2 | Double-welded butt joint | Filler metal in all passes | None required by standard |
| Class 3 | Single-welded butt joint | Filler metal in all passes | Completely radiographed per ASME VIII UW-51 |
| Class 4 | Single-welded butt joint | Pass exposed to inside surface made without filler; other passes with filler | Completely radiographed per ASME VIII UW-51 |
| Class 5 | Double-welded butt joint | Filler metal in all passes | Spot radiographed per UW-52 (≥12 in [300 mm] per 50 ft [15 m]) |
Classes 1, 3, and 4 verify complete seam soundness. Class 5 provides spot verification; Class 2 omits radiography when design stresses permit.
3. Materials, Manufacture, and Welding Rules
Fabrication and welding are governed by Section 6 and Section 9:
- Starting Plate: ASTM A240/A240M plate for the grade specified in Table 1 (Clause 6.1.1).
- Fusion Welding: Full-penetration butt joints by fusion welding per ASME Section IX; procedures and welders qualified to Section IX (Clause 6.2.1).
- Backing Rings: Must share base metal P-Number and be removed after welding; permanent backing is prohibited (Clause 6.2.1).
- Filler Metal & Radiography: Welds made with filler metal except Class 4 inside pass (Clauses 6.2.2.1/6.2.2.2). Single-welded pipe (Classes 3 and 4) must be completely radiographed (Clause 6.2.2.3).
- Weld Crown: Reinforcement ≤1/8 in [3 mm]; concavity prohibited unless total joint thickness meets minimum adjacent base metal (Clause 6.2.3).
- Repairs & Finish: Weld repairs per Section IX, re-examined as original (Clause 6.2.4). Plate grinding permitted if minimum wall is maintained (Clause 9.2); repair welding requires purchaser authorization (Clauses 4.1.8/9.3); repairs deeper than 1/4 wall require pressure testing. Finished pipe must be free of scale and iron particles (Clause 9.4).
4. Heat Treatment Requirements and Stencils
Heat treatment per Table 2 restores corrosion resistance after forming. Clause 6.3.2 governs alternatives and stencils:
| Grade / Condition | Minimum Solution Temperature | Cooling / Quench Method | Marking Stencil |
|---|---|---|---|
| Unlisted austenitic grades (standard) | 1900 °F [1040 °C] | Water quench or rapid cool | Standard A999 |
| Grades 304H, 309S, 309Cb, 310S, 310Cb, 321H, 347H | 1900 °F [1040 °C] | Water quench or rapid cool | Standard A999 |
| UNS N08904 (904L) | 2000 °F [1095 °C] | Water quench or rapid cool | Standard A999 |
| UNS S31254 (254 SMO) | 2100 °F [1150 °C] | Water quench or rapid cool | Standard A999 |
| Final heat treatment under 1900 °F [1040 °C] (per PO) | Below 1900 °F [1040 °C] | Controlled cooling as agreed | “HT” + temp (°F/°C) |
| Pipe from solution-treated plate; no final heat treatment | None after welding | As-welded | “HT-O” |
| Pipe from non-solution-treated plate; no final heat treatment | None after welding | As-welded | “HT-SO” |
Capability to pass ASTM A262 Practice E is demonstrable on request; the test is run only if specified on the order (Clause 6.3.1). Temperatures above 1950 °F [1065 °C] may impair corrosion resistance in stabilized grades (321, 321H, 347, 347H, 348); stabilizing treatment may be specified (Clause 6.4, Supplementary S5).
5. Chemical Composition and Filler Metal Pairings
Under Clause 7.1, plate must conform to ASTM A240/A240M. Filler metal conforms to AWS specifications in Table 1, plate chemistry, or purchaser-approved alloy:
| Plate Grade (ASTM A240) | UNS Designation | AWS Filler Metal Specification (Table 1) | Application Note |
|---|---|---|---|
| 304 | S30400 | AWS ER308, E308 | Standard Cr-Ni match |
| 304L | S30403 | AWS ER308L, E308L | Low carbon for resistance to sensitization |
| 316 | S31600 | AWS ER316, E316 | Molybdenum-bearing for pitting resistance |
| 316L | S31603 | AWS ER316L, E316L | Low carbon with molybdenum |
| 321 | S32100 | AWS ER321, ER347 | Titanium-stabilized base metal |
| 347 | S34700 | AWS ER347 | Niobium-stabilized base metal |
Table 1 footnote C mandates minimum 0.040% carbon for 321H and 347H filler metal. UNS S31655 was added in 2015. Heat analysis is furnished per Section 10. Product analysis is performed per lot of 500 ft [150 m] from plate and weld deposit per ASTM A480 (Section 11).
6. Dimensional Tolerances
Section 8 specifies dimensional limits applicable at any point along the finished pipe:
| Dimension | Clause | Measurement Method | Permissible Tolerance Limit |
|---|---|---|---|
| Outside Diameter (OD) | Clause 8.1.1 | Circumferential measurement at any point | ±0.5% of specified outside diameter |
| Out-of-roundness (Ovality) | Clause 8.1.2 | Difference between major and minor outside diameters | Maximum 1% of specified outside diameter |
| Alignment (Straightness) | Clause 8.1.3 | 10 ft [3 m] straightedge placed on pipe surface | Deviation not to exceed 1/8 in [3 mm] |
| Wall Thickness | Clause 8.1.4 | Measurement at any point | Minimum wall not more than 0.01 in [0.3 mm] under nominal wall |
| Weld Crown Height | Clause 6.2.3 | Height on either outside or inside weld surface | Maximum 1/8 in [3 mm] |
To check standard dimensions and schedule wall thicknesses, see our stainless steel pipe sizes and schedule weight chart.
7. Mechanical Testing, Lot Control, and Pressure Tests
Testing is conducted on a lot basis under Section 15:
- Lot Definition: Same grade, thickness within 3/16 in [4.7 mm], same weld procedure and heat treatment; maximum lot 200 linear ft [60 m] (Clause 15.1).
- Transverse Tension Test: One test across weld seam per lot; tensile strength must meet plate minimum per ASTM A240 (Section 12).
- Guided-Bend Test: One test (two specimens) per lot (Section 13). Wall ≤3/8 in [9.5 mm]: face- and root-bends; >3/8 to <3/4 in [19 mm]: side-bends permitted; ≥3/4 in: both side-bends. Acceptance: no cracks >1/8 in [3 mm]; edge cracks <1/4 in [6.5 mm] ignored.
- Hydrostatic Testing: Each length tested per ASTM A999, held long enough to inspect seam (Clause 15.2).
- Hydro Exemption: By agreement, factory hydro may be omitted in favor of system pressure testing (not lower than design pressure); pipe marked “NH” (Clause 15.3).
8. Radiographic Examination Criteria
Radiographic examination per Section 16 is executed in accordance with ASME BPVC Section VIII, Division 1:
- Classes 1, 3, and 4: All welded joints completely radiographed per Paragraph UW-51.
- Class 5: Spot radiography per Paragraph UW-52 (≥12 in [300 mm] per 50 ft [15 m] of weld seam).
- Class 2: No radiography required by standard.
- Timing: Radiography may be performed before or after heat treatment (Clause 16.1).
For allowable stress and joint efficiency factors, see our pipe pressure rating chart.
9. Supplementary Requirements (S1 through S8)
Supplementary requirements apply only when specified in the purchase order:
| Designation | Requirement Title | Scope and Verification Protocol |
|---|---|---|
| S1 | Product Analysis | Chemical analysis on each length of finished pipe (plate and weld). |
| S2 | Tension and Bend Tests | Transverse tension and guided-bend tests on each pipe length. |
| S3 | Liquid Penetrant Examination | Dye penetrant examination applied to all welded joints. |
| S4 | Ferrite Control in Welds | Ferrite measurement or limit on deposited weld metal. |
| S5 | Stabilizing Heat Treatment | Stabilizing thermal cycle for stabilized grades (321, 321H, 347, 347H, 348). |
| S6 | Intergranular Corrosion Test | Practice E testing per ASTM A262 on plate and weld samples. |
| S7 | Solution Annealing of H Grades | Separate solution annealing for H grades; in-process heat treating is not acceptable. |
| S8 | ASME Section III or VIII Construction | Code construction rules: Certificate of Authorization, Partial Data Report, full-penetration double welds, 200 ft [60 m] lot control. |
10. ASTM A358 Purchase Order Checklist
Section 4 requires orders to define 16 technical items:
- Quantity: Footage, meters, or piece count (4.1.1).
- Product Name: State “electric-fusion-welded pipe” (4.1.2).
- Grade: Designation from Table 1 (4.1.3).
- Class: Pipe class — Class 1, 2, 3, 4, or 5 (4.1.4).
- Dimensions: Specified OD and nominal wall (4.1.5).
- Lengths: Cut or random lengths (4.1.6).
- End Finish: Plain, beveled, or machined per ASTM A999 (4.1.7).
- Plate Defect Repair: Authorization for repair welding on plate (4.1.8).
- Specification: ASTM A358/A358M with year date (4.1.9).
- Special Reqs: Non-standard project requirements (4.1.10).
- Radiography Statement: Statement under Clause 16.4 if RT precedes heat treatment (4.1.11).
- Circumferential Welds: Permissibility per Section 17 (4.1.12).
- Supplementary Options: Selected requirements S1–S8 (4.1.13).
- ASME Code: Applicable construction code (4.1.14).
- Nuclear Class: For ASME Section III, Class 1, 2, or 3 service (4.1.15).
- Certification: Test report requirements per ASTM A999 (4.1.16).
11. Comparison: ASTM A358 vs. ASTM A312
Key differences between ASTM A358 and ASTM A312 include:
- Manufacturing Route: ASTM A358 covers EFW pipe formed from plate with added filler metal. ASTM A312 covers seamless and welded austenitic stainless pipe (see our A312 guide for its manufacturing rules).
- General Requirements: Both specifications are governed by ASTM A999/A999M for general delivery requirements, testing methods, and marking formats.
- Weld Examination: ASTM A358 specifies five radiographic examination classes. ASTM A312 requires hydro or nondestructive electric testing per A999 without radiographic class ratings.
- Wall Thickness Tolerance: ASTM A358 limits wall thinning to 0.01 in [0.3 mm] under nominal wall. ASTM A312 applies ASTM A999 percentage tolerances (−12.5% under-tolerance on nominal wall).
For seamless and strip-welded piping, see our ASTM A312 stainless steel pipe guide.
12. TeCarve Welded Stainless Steel Supply Range
TeCarve is a specialized Chinese stainless steel piping solutions provider and the exclusive factory-direct export channel for two dedicated manufacturing plants in Foshan (welded & decorative tubing) and Wenzhou (seamless & precision tubing). Plant certifications (ISO 9001, ISO 14001, ISO 45001, PED/AD 2000 W0, and marine classifications) are held by the dedicated manufacturing plants — see https://tecarvepipes.com/verify-our-factories/ for details.
The welded stainless steel pipe and tube product page lists TIG, plasma, laser and ERW welded pipe and tube in grades 201, 202, 304, 304L, 316, 316L, 409, 410, 430 and duplex, with outer diameters from 6 mm to 4200 mm, wall thicknesses from 0.5 mm to 120 mm and lengths up to 12 m. ASTM A358 is among the standards listed on that page; confirm class, grade and radiography requirements with us at inquiry stage.
Each order is supplied with an EN 10204 3.1 mill test certificate issued by the producing plant. See our EN 10204 3.1 mill test certificate guide.
13. Frequently Asked Questions (FAQ)
What is the primary difference among the five classes in ASTM A358?
The five classes define joint type and radiography: Class 1 (double-welded, complete RT); Class 2 (double-welded, no RT); Class 3 (single-welded, complete RT); Class 4 (single-welded, inside pass may be made without filler metal, complete RT); and Class 5 (double-welded, spot RT at least 12 in [300 mm] per 50 ft [15 m] of weld seam).
When is ASTM A358 Class 1 required instead of Class 2 or Class 5?
Class 1 is specified when construction codes (ASME Section VIII, Division 1 or ASME B31.3) mandate joint efficiency E = 1.00 for severe pressure or corrosive service. Class 2 requires lower design stresses without radiography, while Class 5 spot radiography permits E = 0.85.
Can ASTM A358 pipe be supplied without factory hydrostatic testing?
Yes. Under Clause 15.3, purchaser and producing plant may agree to defer hydrostatic testing to a system pressure test (not lower than design pressure). Such pipe must be stenciled “NH” (No Hydro).
What do the heat-treatment stencils “HT”, “HT-O”, and “HT-SO” indicate?
Under Clause 6.3.2, “HT” marks final heat treatment below 1900 °F [1040 °C] plus temperature; “HT-O” marks pipe from solution-annealed plate without subsequent heat treatment; and “HT-SO” marks pipe from non-solution-treated plate without subsequent heat treatment.
How does ASTM A358 differ fundamentally from ASTM A312?
ASTM A358 covers plate-fabricated EFW pipe with added filler metal across five radiographic classes. ASTM A312 covers seamless pipe from billets or welded pipe from strip without filler metal. Both reference ASTM A999/A999M for general requirements.
What radiographic acceptance standards govern ASTM A358 weld seams?
Radiography follows ASME BPVC Section VIII, Division 1. Classes 1, 3, and 4 follow complete radiography under Paragraph UW-51. Class 5 spot radiography follows Paragraph UW-52 (at least 12 in [300 mm] per 50 ft [15 m] of weld seam).
Summary based on ASTM A358/A358M-15; later editions may differ — refer to the purchased standard for the full text.